
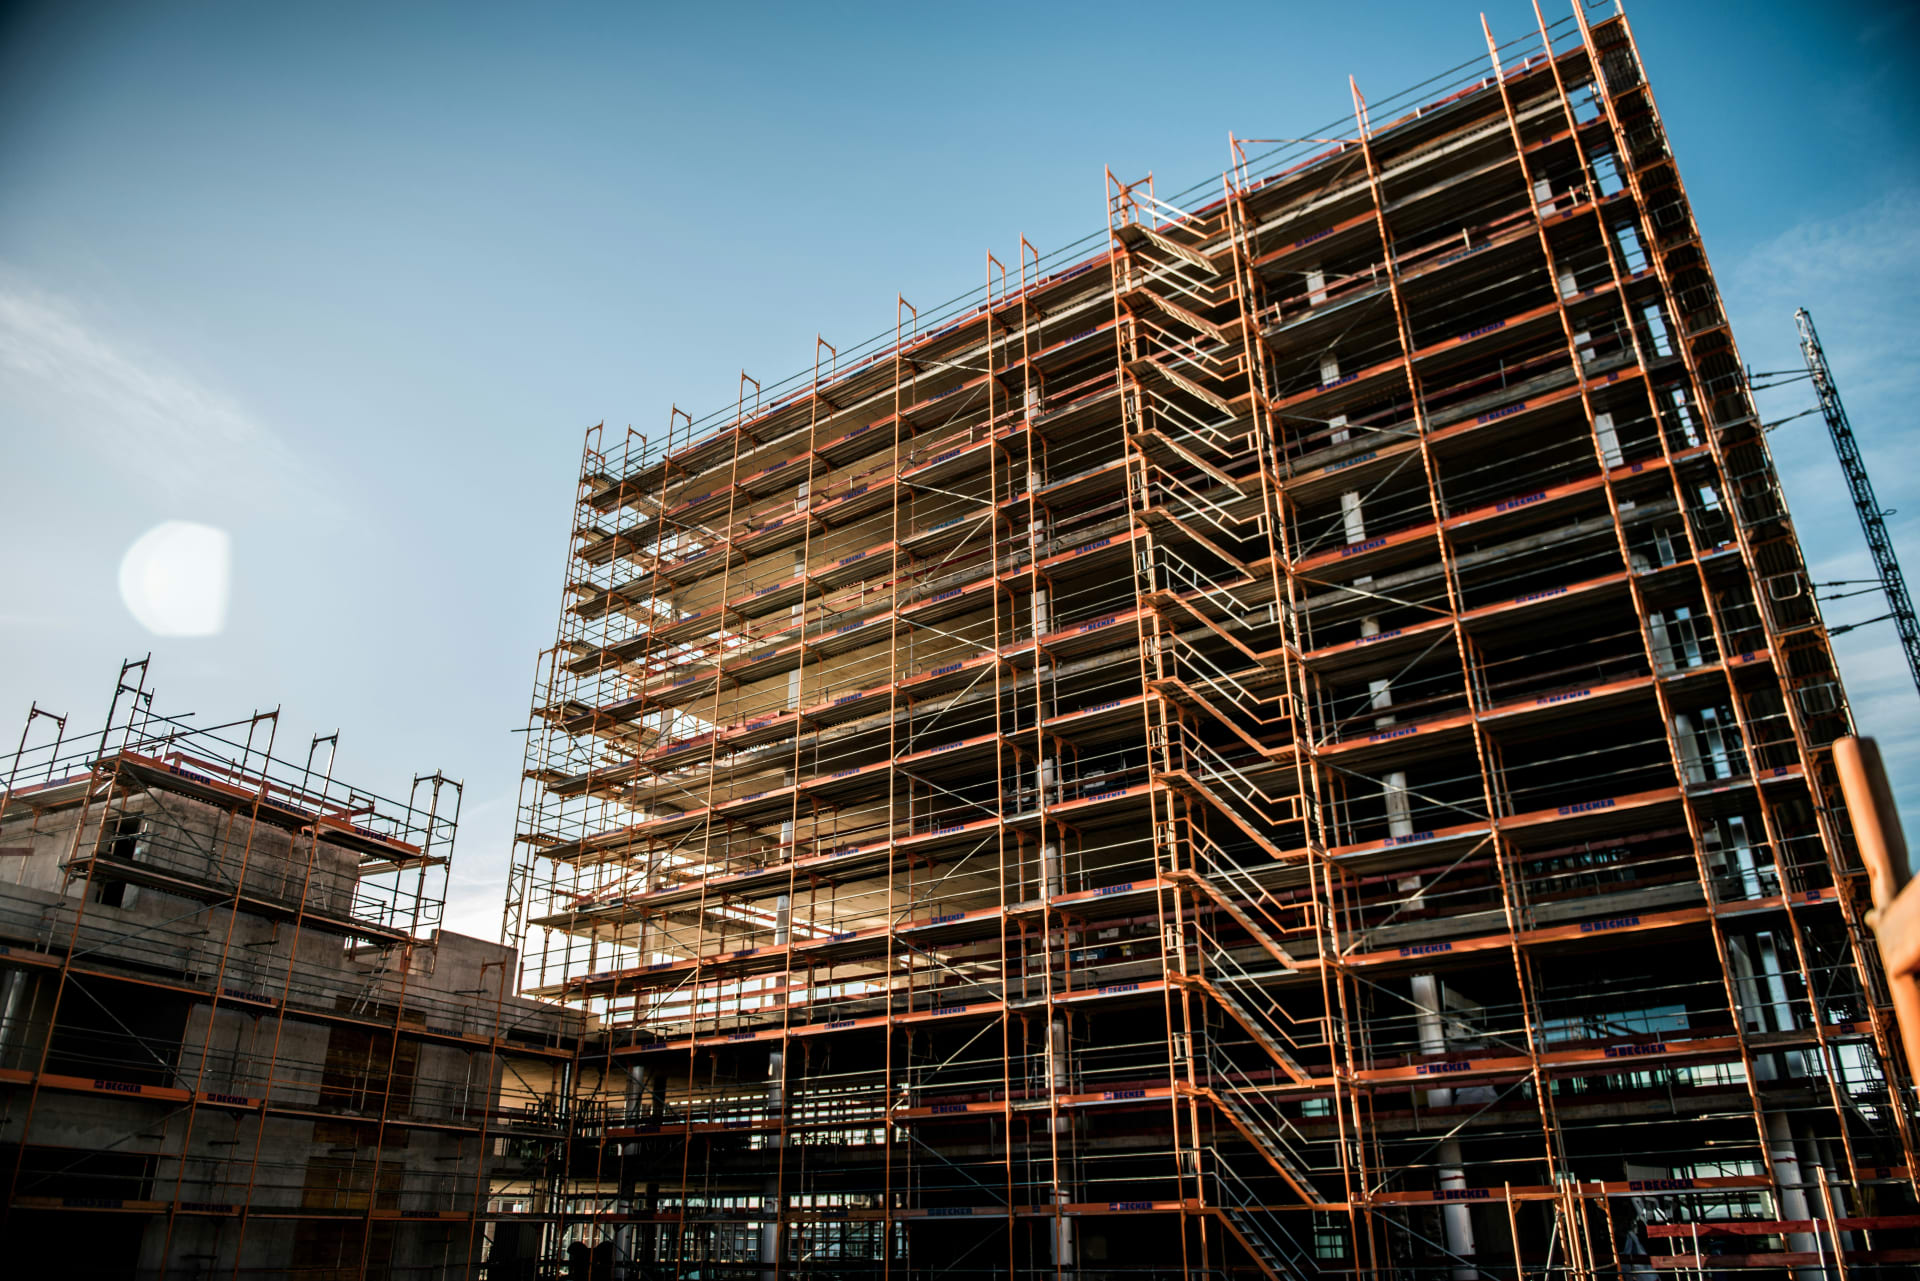
Cuplock Scaffolding System Manufacturer
Cuplock makes its connection with two cups rather than a rosette. A bottom cup is welded to the standard, and a top cup slides down over up to four ledger blades and locks them all with a single hammer blow.
Cuplock makes its connection with two cups rather than a rosette. A bottom cup is welded to the standard, and a top cup slides down over up to four ledger blades and locks them all with a single hammer blow. On a rectangular elevation that is the fastest modular connection in use, because one action secures four members and there is nothing loose to hold, drop or lose. KEAA International manufactures nine Cuplock components in Ludhiana, India, from steel to EN 10025 and EN 10219, hot dip galvanized to DIN EN 1461 in our own plants. The system is specified where erection speed matters and the geometry is regular, which describes most building facades and most birdcage support work.
What a Cuplock scaffold is built from
Standards carry the bottom and top cups at fixed centres. Ledgers with ledger blades lock into the cups and span horizontally. Truss ledgers span openings where a standard cannot be landed, for instance over a doorway or a vehicle access. Diagonal braces triangulate the bay. Side brackets widen the working platform and Cuplock ladder brackets carry access between lifts.
Why the cup weld is the component that matters
In a Cuplock scaffold the load path runs through the cups, so the weld that fixes the bottom cup to the standard is the part carrying the connection. It is not a materials question, it is a welding quality question, and it is not visible once galvanized. Our welding is carried out by welders certified to EN 1090-2 and EN 3834-2, accredited by SLV Germany, and carried out in house rather than subcontracted.
Where Cuplock beats Ringlock, and where it does not
On a straight elevation Cuplock is faster to erect and strike, because one blow does the work of four connections and the part count per bay is lower. Where the structure curves or the bracing has to run at an angle the cups cannot reach, Ringlock is the better fit. Neither is universally correct, which is why plenty of contractors hold both and choose per job.
At a glance
| Components manufactured | Standards, top and bottom cups, ledgers, ledger blades, truss ledgers, diagonal braces, side brackets, ladder brackets |
|---|---|
| Steel specification | EN 10025 and EN 10219 |
| Corrosion protection | Hot dip galvanized to DIN EN 1461 |
| Connection | Top and bottom cup, up to four ledgers per node |
| Welding | Welders certified to EN 1090-2 and EN 3834-2, SLV Germany |
| Manufacturing location | Ludhiana, Punjab, India |
Standards
- EN 10025 / EN 10219
- The structural steel and hollow sections the components are made from.
- DIN EN 1461
- Hot dip galvanized coatings, applied in our own plants.
- EN 1090-2 / EN 3834-2
- Execution of steel structures and fusion welding quality, certified through SLV Germany.
Where it is used
- Building facades and refurbishment on regular elevations
- Birdcage scaffolds and internal support work
- General construction access
- Support and falsework where speed over a repeated area decides
Common questions
One hammer blow on the top cup locks up to four ledgers into the node at once, and there are no loose couplers to hold or drop. Across every bay and every lift, that difference compounds.
Spanning an opening where a standard cannot be landed, such as over a doorway or vehicle access. It carries the load across to the standards on either side.
No. The connections are different and not interchangeable. A scaffold is built from one system.
Request a quotation
Send the sizes, finish, standard and quantities you need. We manufacture in our own plants in Ludhiana, India and export to more than 42 countries, so quotations are prepared for container volumes as readily as for single lines.